 English
 Español
 Català
 Deutsch
 Português
 Français
 Italiano
 Turkish
 Czech
 Chinese-Simplified


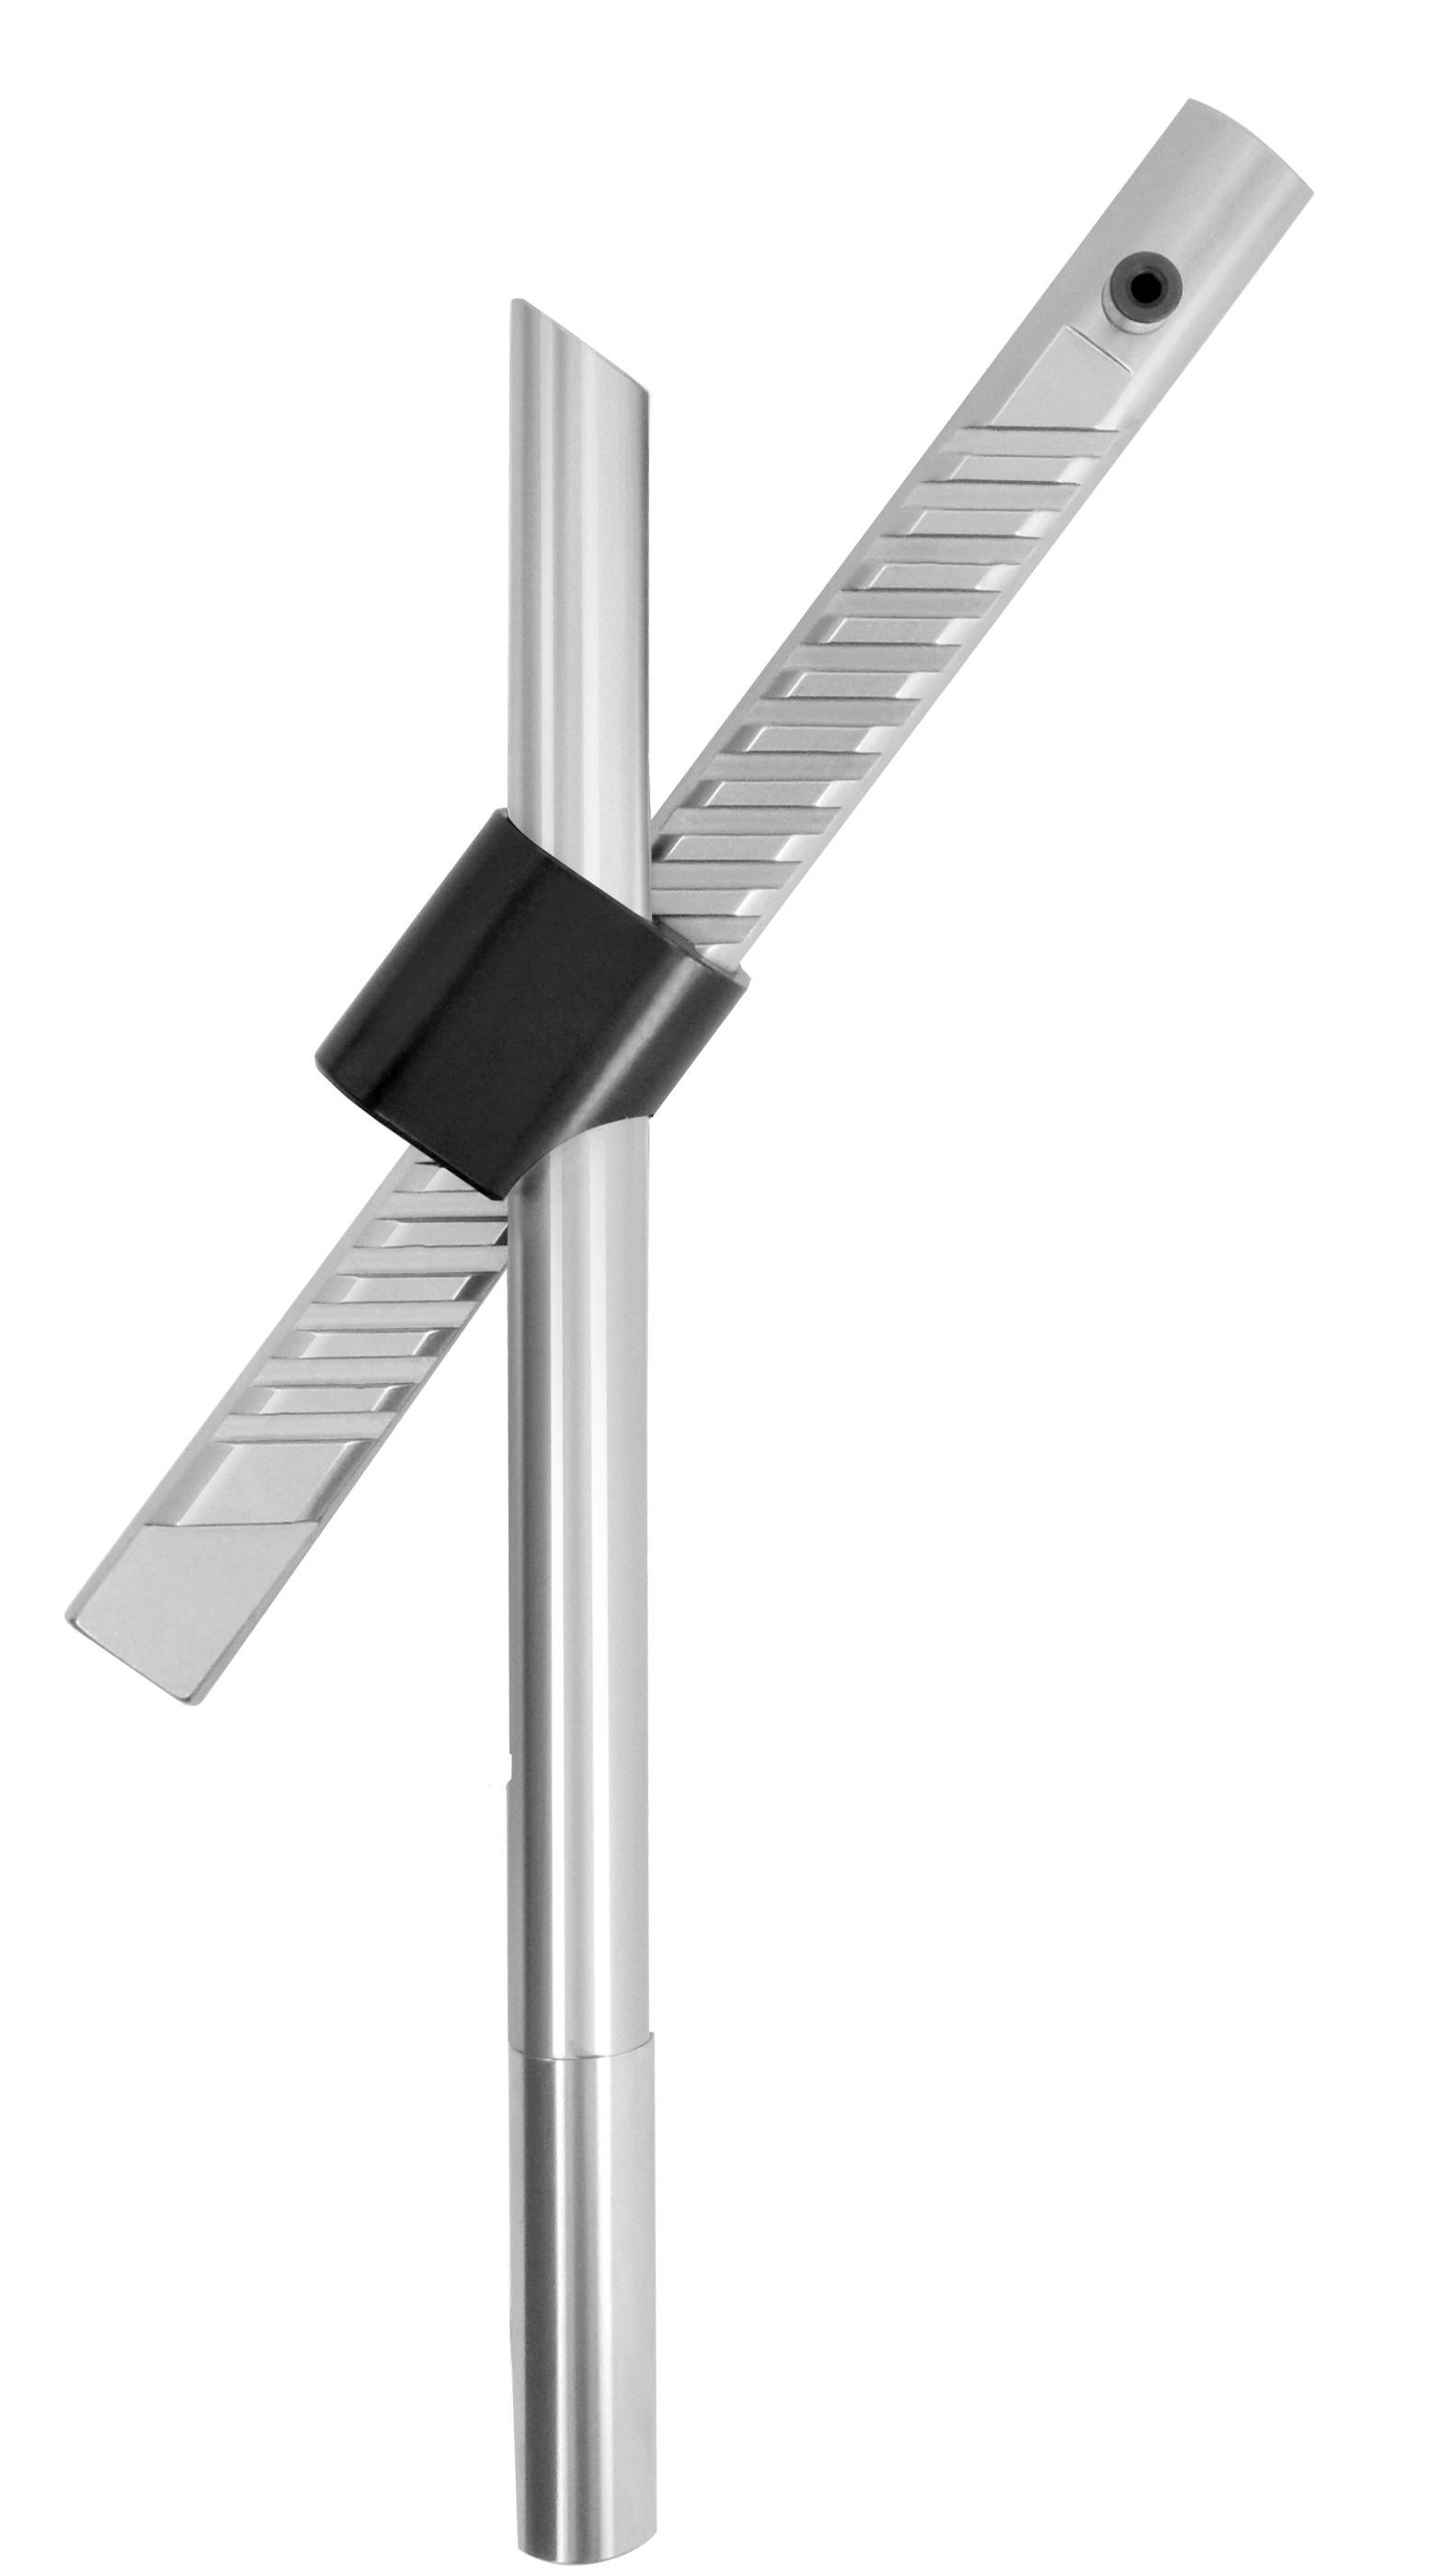
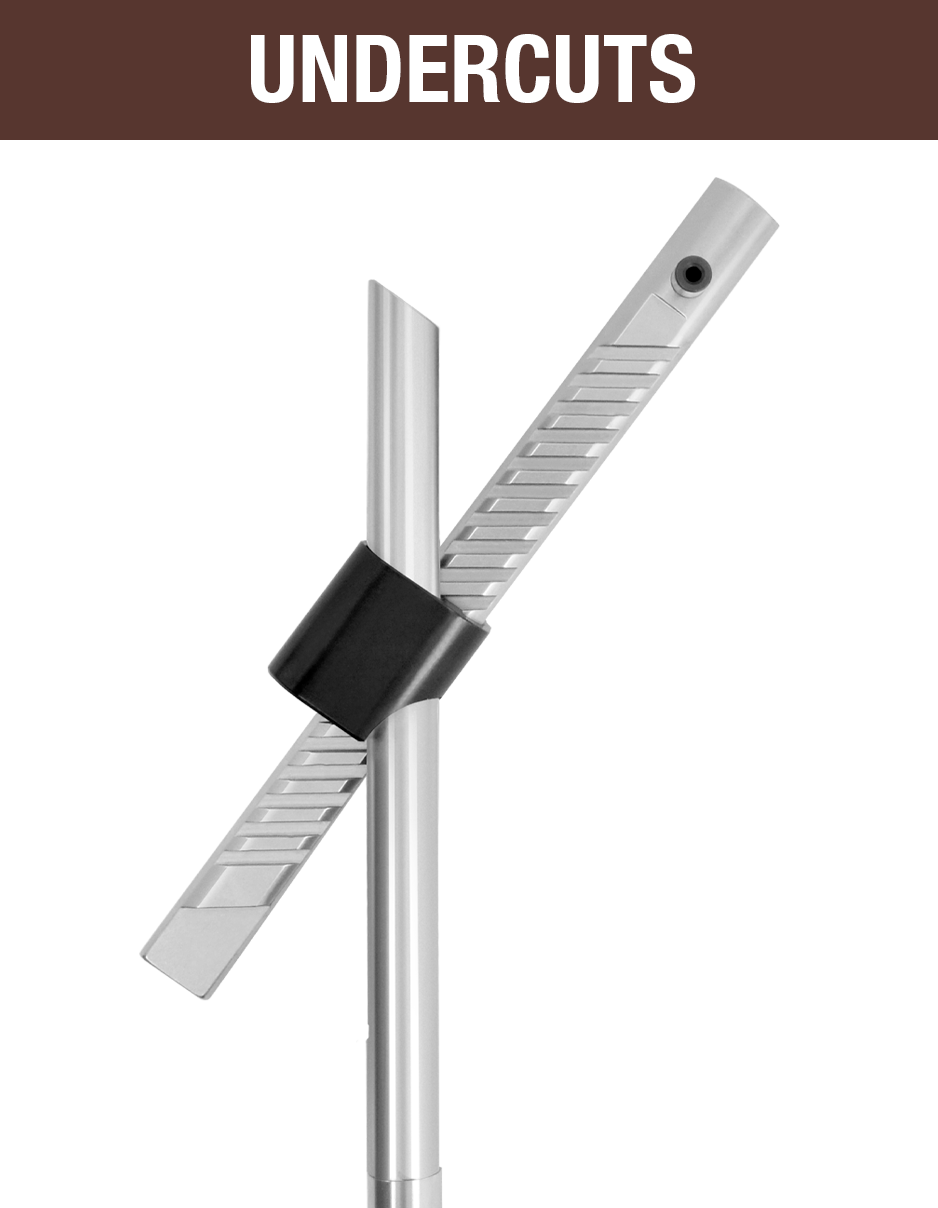
Since 1995, CUMSA has led the development of Sprung Core solutions for releasing small undercuts in injection molds.
The new PZ represents the culmination of more than three decades of innovation and continuous improvement, combining the key advantages of the PX and PW models into a single, optimized product:
The PZ represents the natural evolution of our sprung core technology, delivering greater efficiency while simplifying selection and application.
The result is a more versatile, efficient, and cost-effective sprung core, engineered to meet today’s mold making challenges.
Correctly installed sprung cores (following our catalogue installation instructions) can produce more than 1 million parts.
The opening of the sprung cores is a radial movement. Due to this, at the edge of the stroke, the opening is 4.5mm (0.177”).
Welding is not recommended on any of the sprung core products. Welding exposes them to high temperatures which can affect the treated areas, and therefore the characteristics of the spring steel.
In the catalogue page (view PDF), all the necessary dimensions and tolerances required for assembly are shown, as well as the correct installation procedure.
The maximum working temperature is 150°C (302°F).
The sprung cores have a flat on the side of the shaft to position them, this must be used to avoid the sprung core turning while fixing it to the ejector plates and therefore preventing it to function in a forced position.
We only recommend treatments using Balinit C, as this is the only one that is applied at temperatures below the 150°C / 302°F, therefore preventing changes to the properties of the spring steel. Other treatments like nitriting, TIN, PVD…. are not recommended as they can reduce the sprung core life.
Yes, it is possible, but always maintaining at least 3º.
Yes, we recommend a minimum of 2º per side.
Yes, because the 6º angle supports the shut off of the head in its location hole.
It must have a minimum of 5mm plus the part detail in the C dimension of the sprung core.
Yes, it is very important to give draft on the undercut, for the PZ => 3º.
The shaft has to be keyed.
45mm.
18mm.
Yes, if the sprung core is correctly keyed, therefore when returning to its hole will not suffer any pressure on the spring area.
Please sign in first.
Sign in