 Català
 Español
 Deutsch
 Português
 Français
 Italiano
 Turkish
 Czech
 English
 Chinese-Simplified
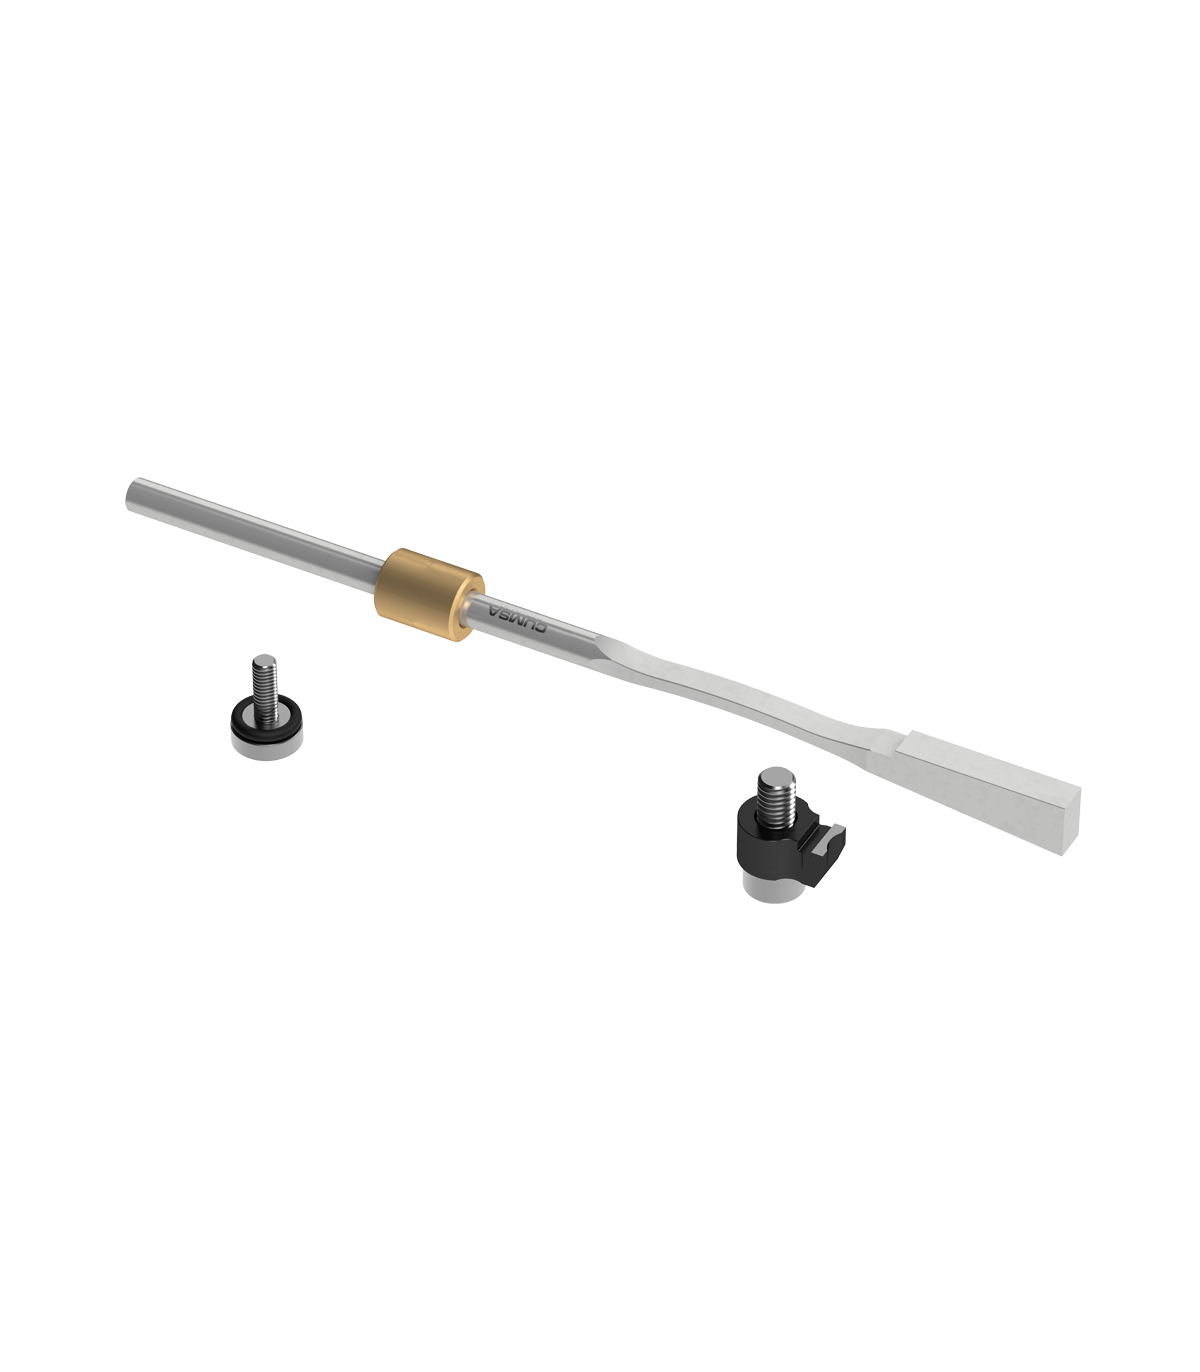

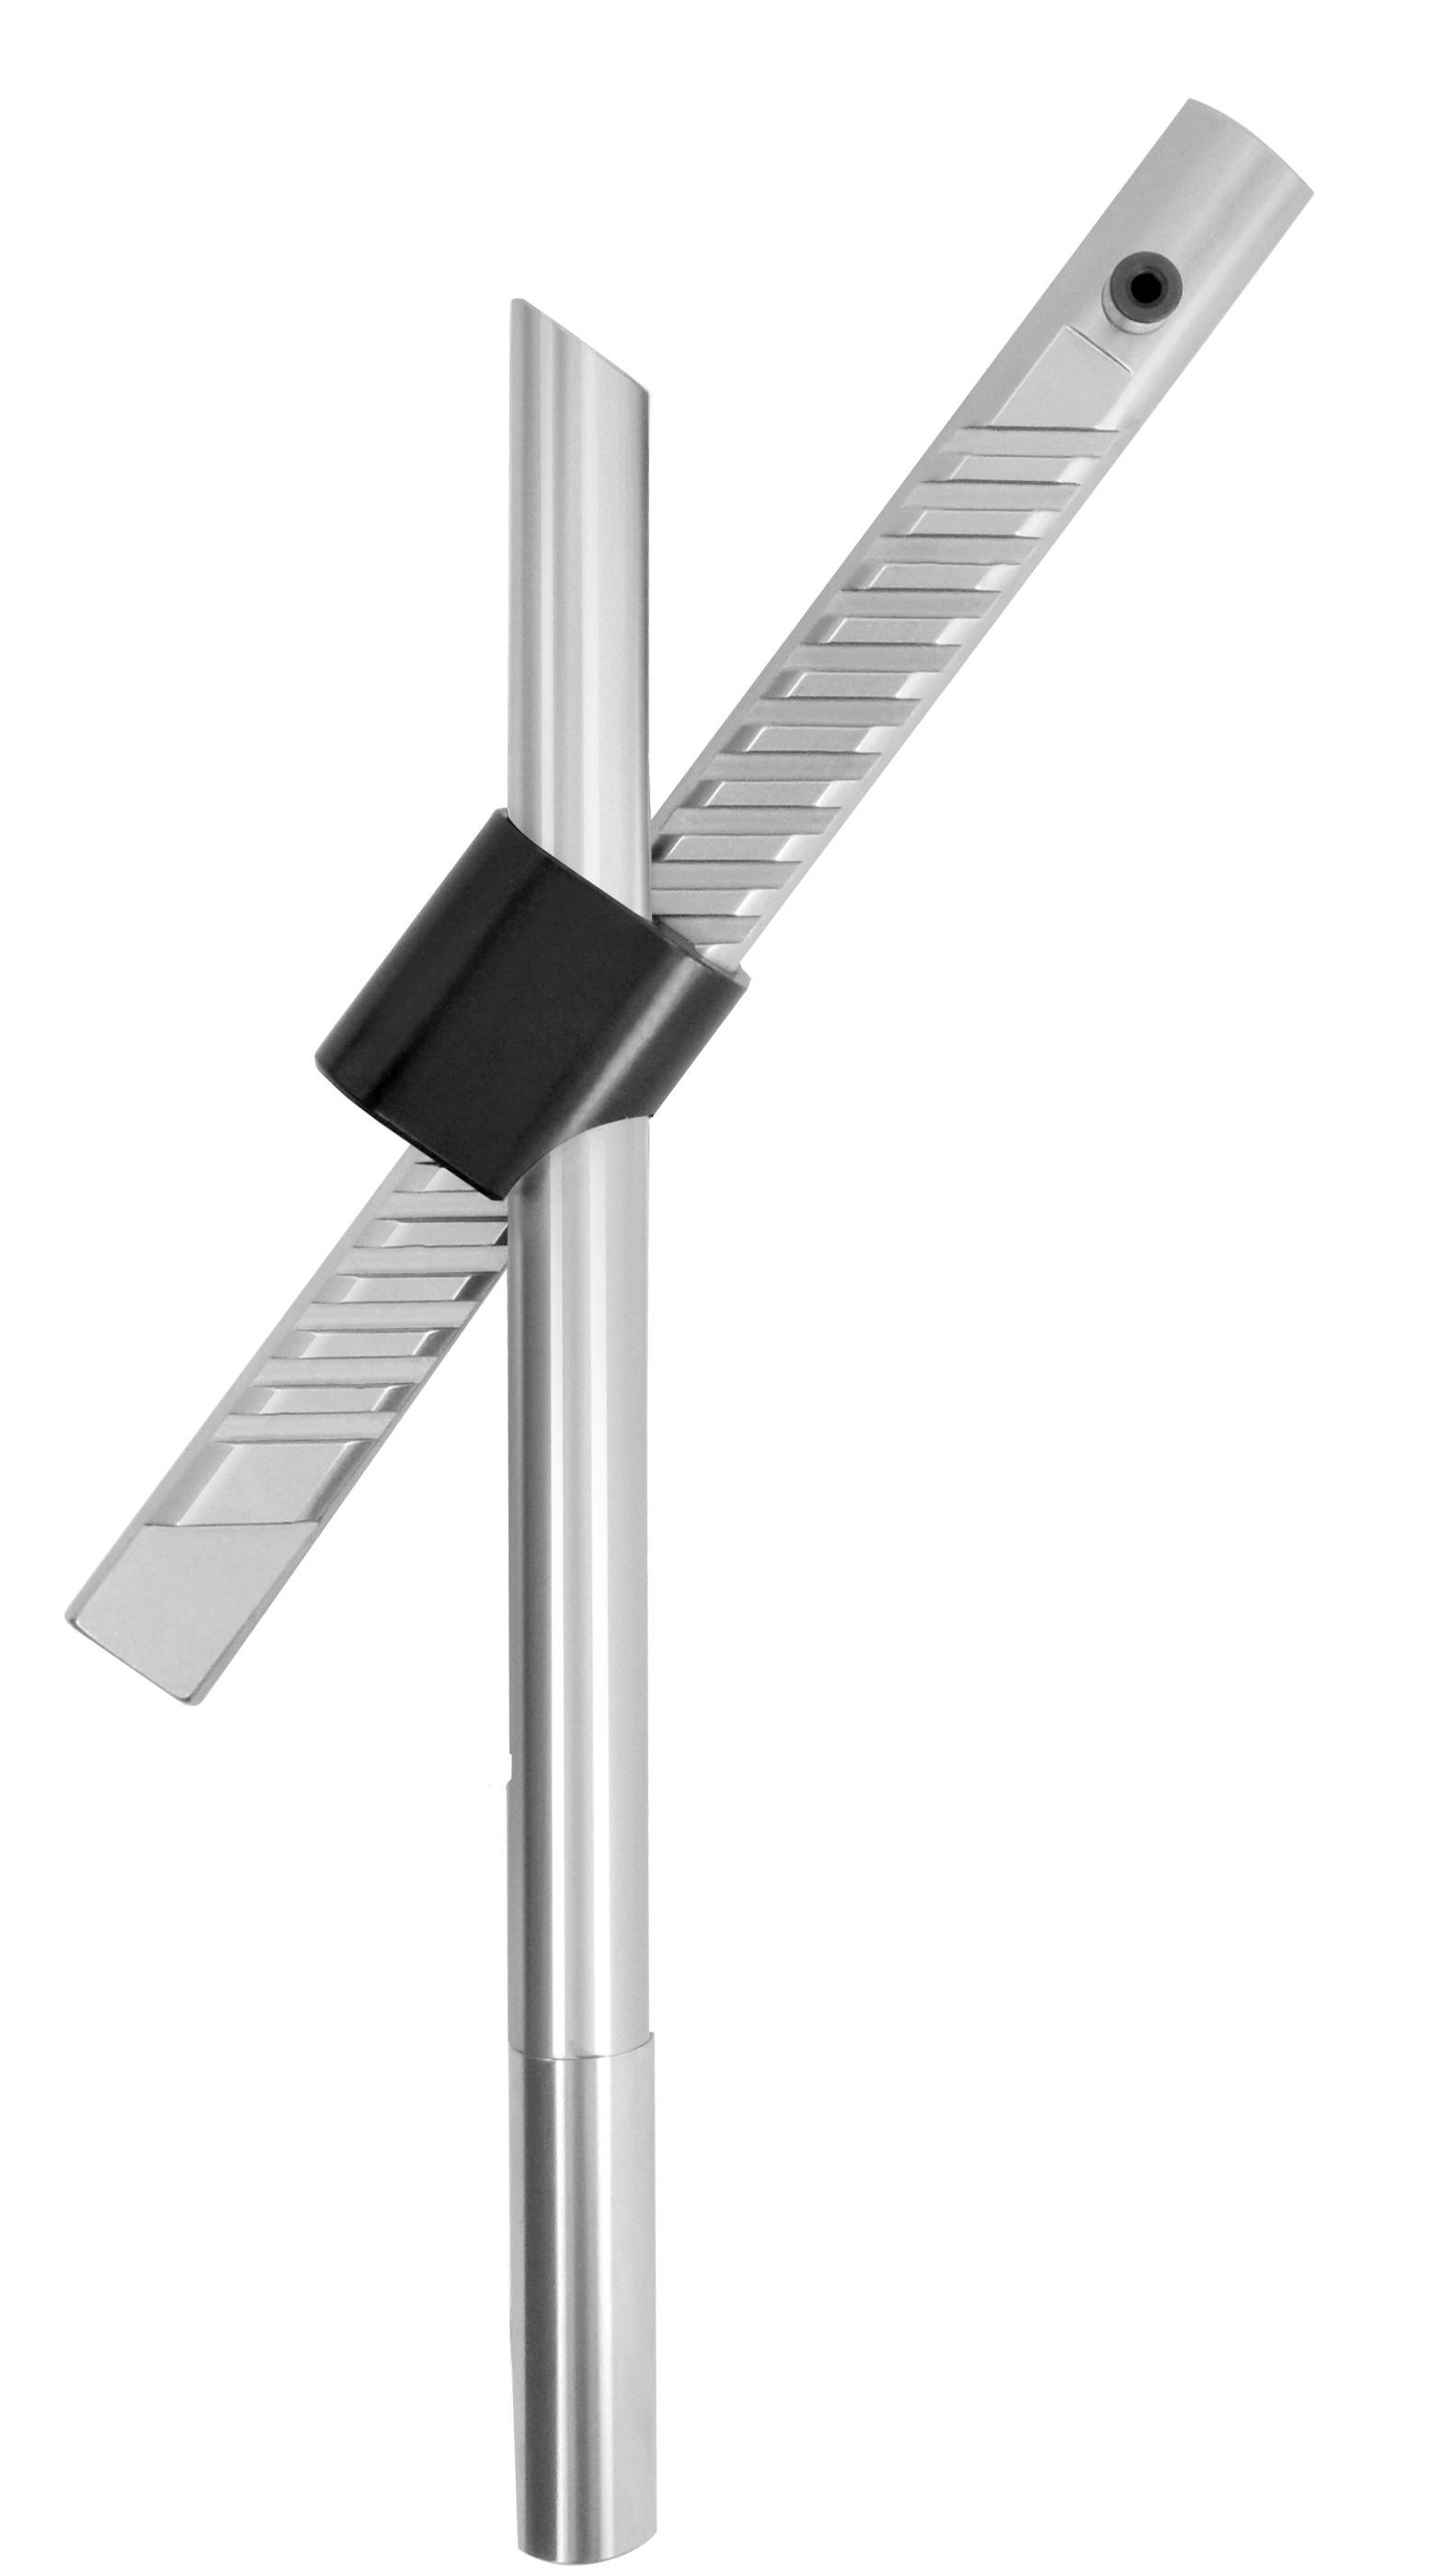
Des de 1995, CUMSA lidera el desenvolupament de solucions de pinces planes per l’expulsió de negatius petits en motlles d’injecció.
El nou PZ representa la culminació de més de tres dècades d’innovació i millora contínua, combinant els principals avantatges dels models PX i PW en un sol producte optimitzat:
El PZ representa l’evolució natural de la tecnologia de pinces planes, oferint més eficiència al mateix temps que simplifica la selecció i l’aplicació.
El resultat és una pinça més versàtil, eficient i rendible, dissenyada per a fer front als reptes actuals de la fabricació de motlles.
Correctly installed sprung cores (following our catalogue installation instructions) can produce more than 1 million parts.
L'obertura de les pinces és un moviment radial. A causa d'això, al límit del recorregut, l'obertura és de 4,5 mm (0,177").
Welding is not recommended on any of the sprung core products. Welding exposes them to high temperatures which can affect the treated areas, and therefore the characteristics of the spring steel.
In the catalogue page (view PDF), all the necessary dimensions and tolerances required for assembly are shown, as well as the correct installation procedure.
The maximum working temperature is 150°C (302°F).
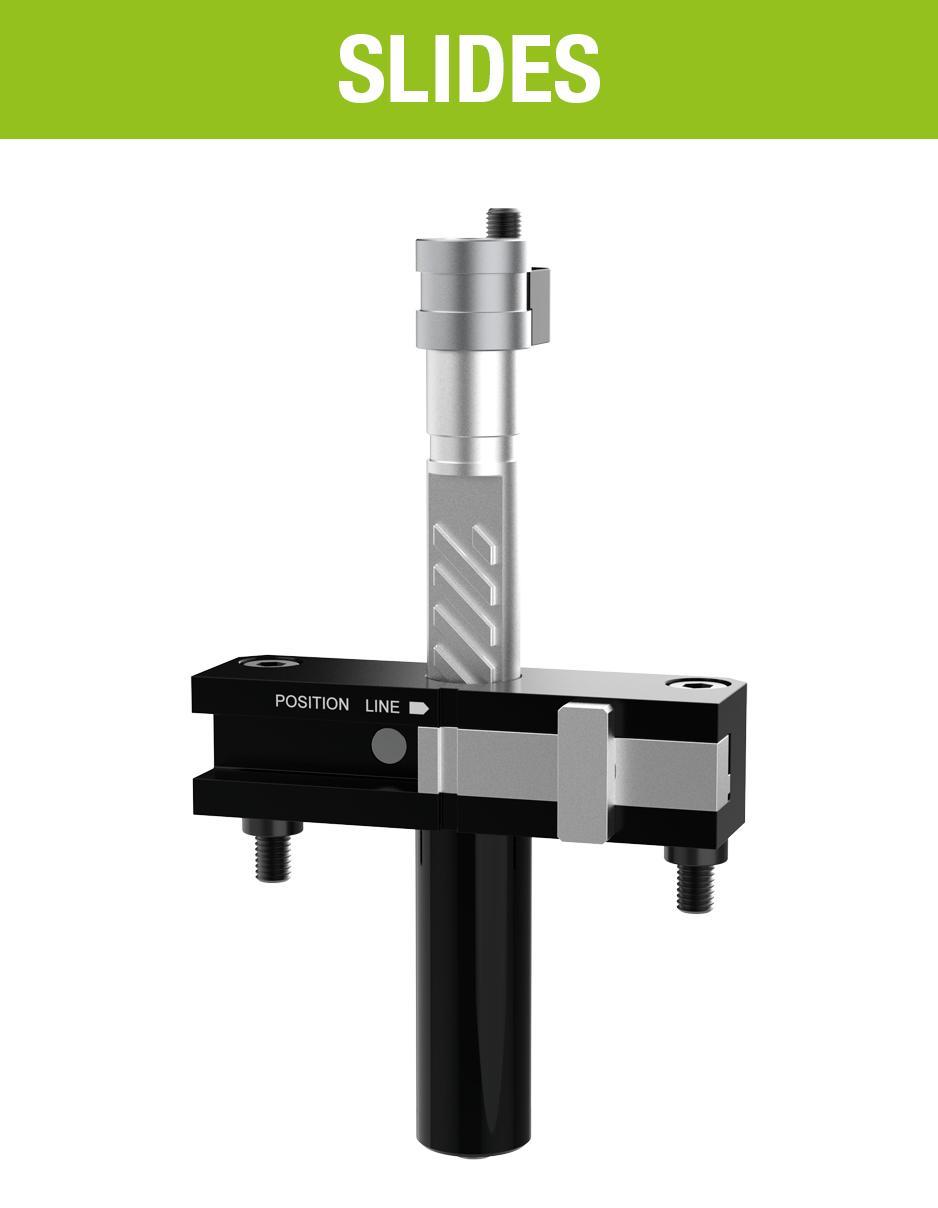
The sprung cores have a flat on the side of the shaft to position them, this must be used to avoid the sprung core turning while fixing it to the ejector plates and therefore preventing it to function in a forced position.
We only recommend treatments using Balinit C, as this is the only one that is applied at temperatures below the 150°C / 302°F, therefore preventing changes to the properties of the spring steel. Other treatments like nitriting, TIN, PVD…. are not recommended as they can reduce the sprung core life.
Yes, it is possible, but always maintaining at least 3º.
Yes, we recommend a minimum of 2º per side.
Yes, because the 6º angle supports the shut off of the head in its location hole.
It must have a minimum of 5mm plus the part detail in the C dimension of the sprung core.
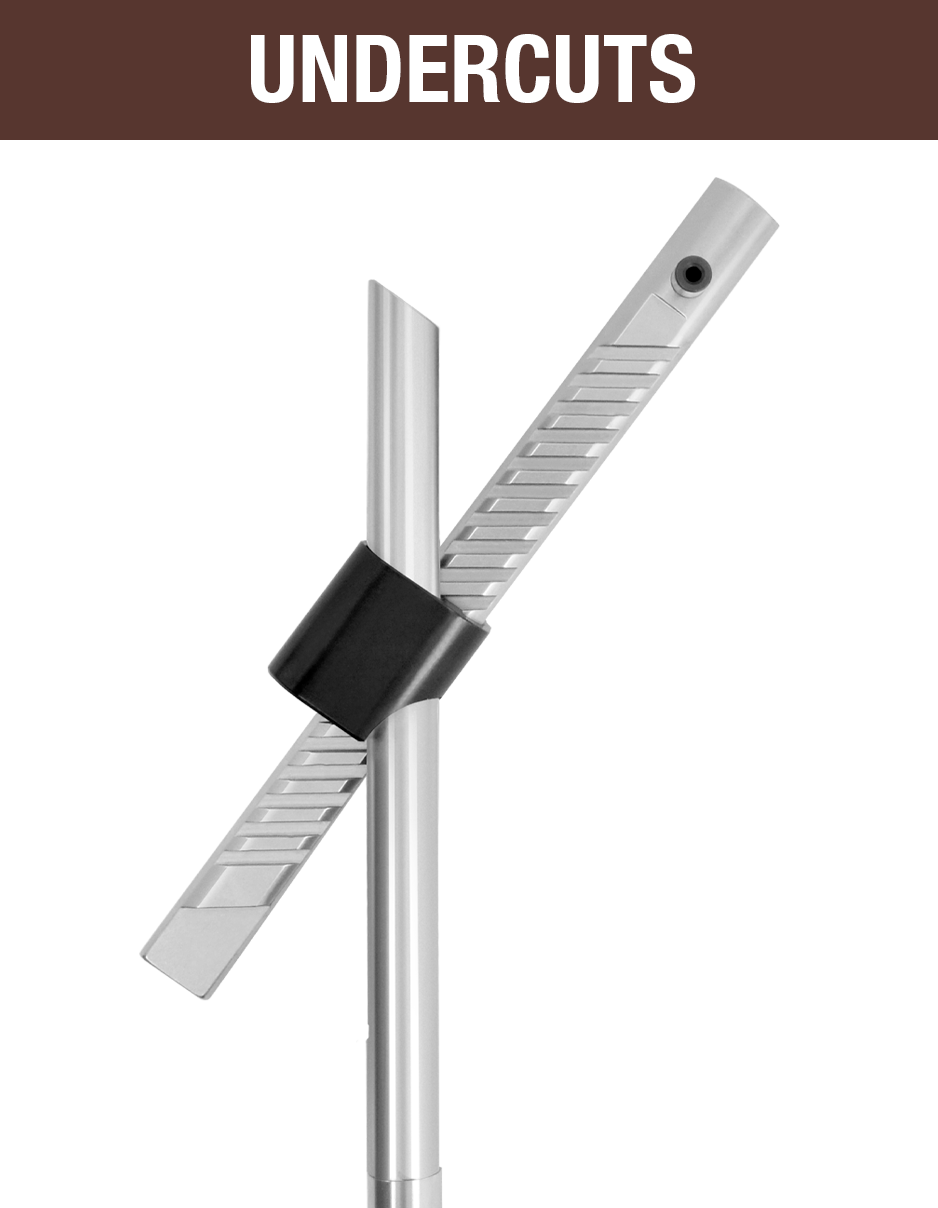
Yes, it is very important to give draft on the undercut, for the PZ => 3º.
The shaft has to be keyed.
45mm.
18mm.
Si, sempre que la pinça es posicioni correctament amb l'antigir, que evitarà que la zona de la molla pateixi pressions al tornar al seu allotjament
Please sign in first.
Registra't